
Product Introduction
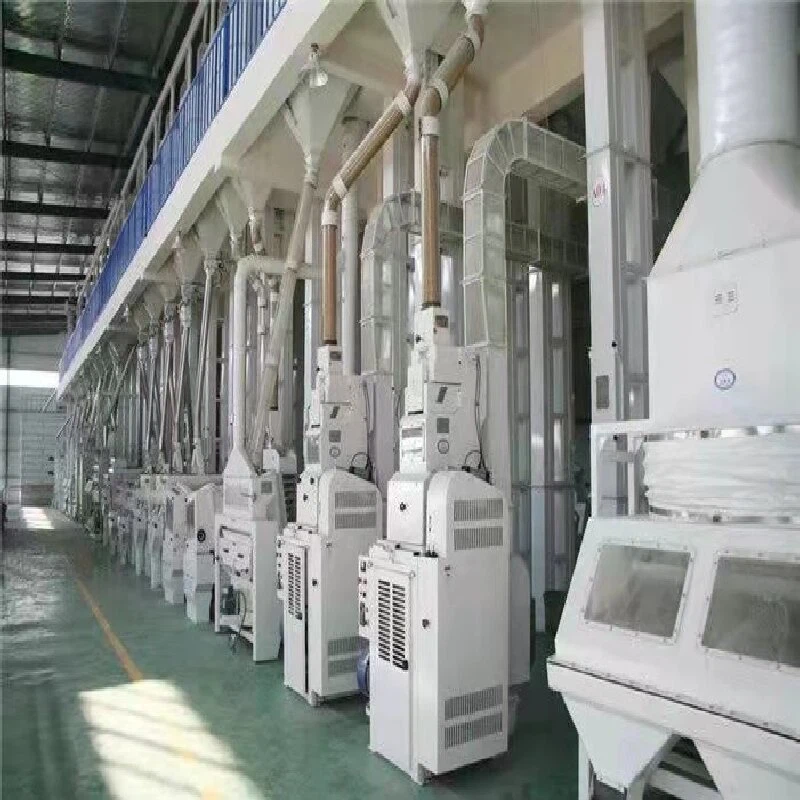
Designed specifically for high-volume rice processing lines, our fully automatic new durable elevator stands as a robust, high-efficiency conveying solution engineered to streamline the transfer of raw rice, semi-processed grains, and finished rice products across different stages of milling and packaging. Unlike conventional elevators prone to wear and downtime, this model integrates full automation with heavy-duty construction to minimize manual intervention, boost throughput, and cut operational costs for rice mills of all scales. Its intelligent design ensures gentle handling of rice grains to prevent breakage and maintain product quality, making it an indispensable core component for modern rice processing facilities seeking reliability and productivity.
Product Material
1.Hopper & Bucket: High-quality cold-rolled steel plate with electrostatic spray coating, offering excellent corrosion resistance and impact resistance to withstand long-term contact with rice grains and dust.
2.Conveyor Belt/Chain: Industrial-grade rubber belt (for light-duty applications) or carbon steel roller chain (for heavy-duty scenarios), featuring high tensile strength and low elongation to ensure stable conveying.
3.Frame & Support Structure: Galvanized steel profiles, enhancing rust prevention and structural rigidity to support continuous operation under heavy loads.
4.Drive System Components: Cast iron gearbox and stainless steel motor housing, suitable for the dusty, humid environment of rice processing plants.
Product Advantages

Newly upgraded high-efficiency and multi production hoist
The core advantages of rice processing equipment elevators include high efficiency, convenience, precise control, energy conservation, environmental protection, as well as improvements in processing efficiency and rice quality. These benefits have solidified the importance of rice processing equipment in the modern grain processing industry, driving its modernization.
1. The high efficiency and convenience of rice processing equipment are among its most prominent features. This equipment is compact, easy to operate, and can swiftly complete the entire process from rice harvesting to precise processing. Compared to traditional manual methods, mechanized equipment significantly reduces human involvement and boosts production efficiency.
2. Precise control is another key advantage. The advanced control systems used in rice processing equipment ensure the accuracy and quality of the processing. This precise control not only enhances the quality of the rice but also guarantees that each grain is meticulously processed to meet consumer expectations.
3. Energy conservation and environmental protection are also important benefits of rice processing equipment. By utilizing advanced energy-saving technologies, this equipment effectively reduces energy consumption and minimizes environmental impact. With the continued advancement of technology, rice processing equipment is becoming more energy-efficient, aligning with the goals of sustainable development.
4. Improving processing efficiency and ensuring rice quality are the core functions of rice processing equipment. Mechanized processing significantly boosts efficiency and reduces labor costs, while precision processing ensures higher rice quality and enhances its nutritional value.
Craftsmanship & Technology
1.Precision Bucket Mounting Technology: Adopts a high-precision welding and riveting process to ensure buckets are firmly fixed on the conveyor belt/chain, eliminating the risk of bucket detachment during high-speed operation.
2.Intelligent Speed Regulation System: Equipped with a variable frequency drive (VFD) to adjust conveying speed according to upstream and downstream equipment capacity, achieving seamless synchronization and reducing grain breakage rate to below 0.5%.
3.Sealed Dust-Proof Design: The fully enclosed housing structure prevents dust leakage and rice spillage, meeting environmental protection standards and reducing cleaning workload.
4.Wear-Resistant Reinforcement Treatment: Key wear parts such as bucket edges and hopper liners are treated with surface hardening to extend service life by 30% compared to standard products.
5.Automatic Fault Alarm System: Integrated with sensors to monitor motor temperature, chain tension, and bucket operation status; triggers real-time alarm and automatic shutdown in case of abnormalities to avoid equipment damage.
Application Fields
This fully automatic durable elevator is widely applied in various links of the rice processing industry, including:
1.Raw rice storage and feeding: Conveying bulk rice from silos to cleaning and destoning machines.
2.Intermediate processing transfer: Transporting rice between husking, milling, polishing, and grading equipment.
3.Finished product packaging: Delivering polished rice to weighing and packaging lines.
4.Auxiliary material handling: Conveying bran and other by-products to storage areas for secondary processing.
It is also suitable for small and medium-sized grain processing plants dealing with wheat, corn, and soybeans, with minor adjustments to bucket specifications.
FAQ
Q: What is the maximum lifting height of this elevator?
A: The standard model supports a lifting height of 3–15 meters. For higher conveying needs (up to 25 meters), we can customize the frame structure and drive system to ensure stability and safety.
Q: How to reduce rice grain breakage during conveying?
A: Our elevator is equipped with a variable frequency drive to control conveying speed, and the buckets are designed with a smooth, curved edge for gentle loading and unloading. Additionally, we can install soft rubber liners in the hopper to further reduce impact on grains.
Q: Is this equipment suitable for humid environments?
A: Yes. The frame and key components are made of galvanized or spray-coated steel, and the motor uses a waterproof and dustproof enclosure (IP54 rating), making it suitable for the humid, dusty working conditions of rice mills.
Hot Tags: fully automatic new durable elevator, China fully automatic new durable elevator manufacturers, suppliers, factory, rice processing technology, modular rice processing line, environmentally friendly rice processing machines, rice processing for industrial use, rice processing with multiple functions, rice processing in urban areas


